resources
Silicone and Elastomeric Overmoulding for IoT Devices: FVG's Capabilities

Published on 15th Sept 2026
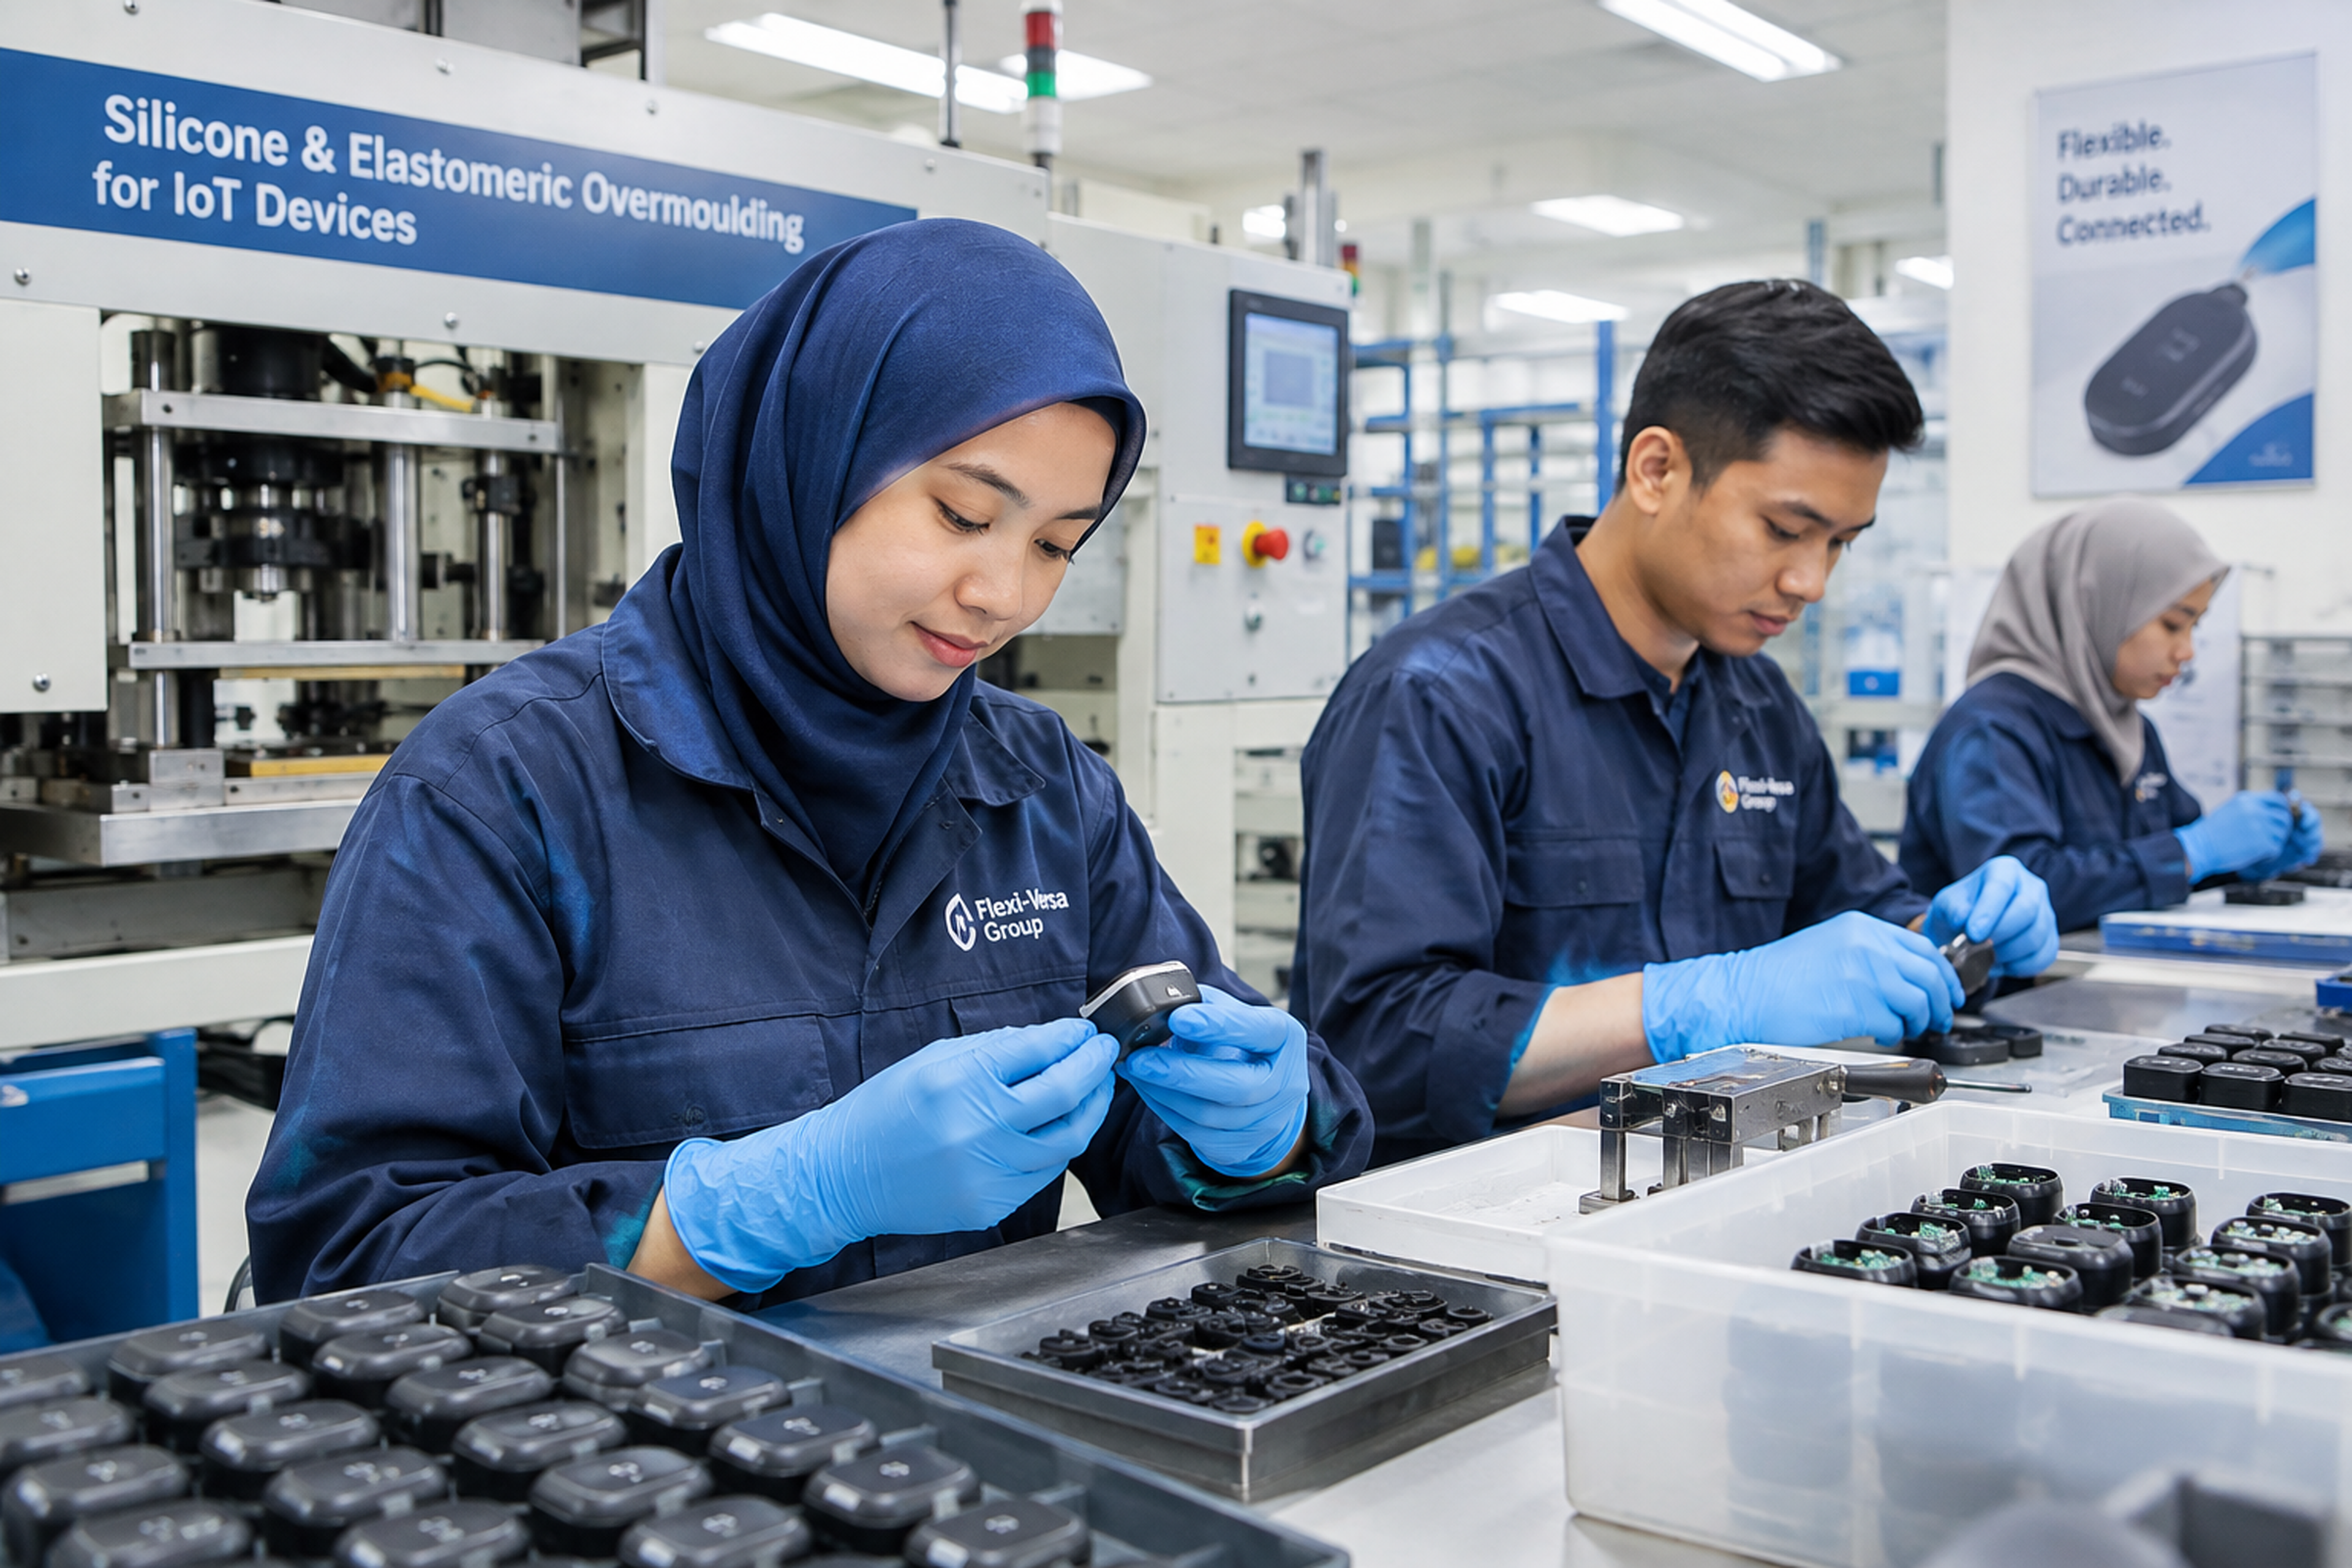
Flexi Versa Group (FVG) provides both silicone (LSR) and broader elastomeric overmoulding for IoT and connected devices, combining precision moulding with in-house PCBA manufacturing under a single vertically integrated roof.
IoT hardware engineers face a recurring dilemma when specifying overmoulded enclosures: finding a manufacturer who can bond a flexible elastomeric layer to populated PCBs without farming out either the electronics or the moulding. Misaligned tolerances, disconnected supply chains, and incompatible process temperatures are the usual casualties of splitting those two scopes.
FVG solves that problem by holding both capabilities in-house. The same facility that assembles your IoT PCB can overmould the protective silicone or elastomeric layer, validate the IP rating, and ship a finished sub-assembly. This article breaks down what that capability actually covers: materials, process specs, supported applications, and the compliance framework behind it.
Overmoulding is a co-moulding process in which an elastomeric material is injection-moulded directly over a rigid substrate, such as a thermoplastic housing, a metal insert, or a populated printed circuit board assembly (PCBA). The result is a single bonded component that combines structural rigidity with the protective and functional properties of the elastomer layer.
For IoT devices, this matters for three specific reasons:
Environmental sealing: Overmoulded elastomeric gaskets and enclosures achieve consistent IP67 and IP68 ratings, protecting electronics from dust, moisture, and submersion. Mechanically assembled gaskets carry a significantly higher field failure rate under thermal cycling compared to chemically bonded overmoulded seals.
Shock and vibration resistance: Industrial IoT sensors deployed in factories, logistics hubs, or outdoor infrastructure are subject to continuous mechanical stress. A bonded elastomeric layer absorbs impact energy that would otherwise fracture solder joints or crack housings.
Form factor integration: Overmoulding eliminates secondary assembly steps, screws, and adhesive bonds, reducing part count and improving long-term reliability in miniaturised connected devices.
Key distinction: Silicone overmoulding (using Liquid Silicone Rubber, or LSR) and elastomeric overmoulding are related but not identical. LSR is a subset of the broader elastomer family, chosen specifically for applications requiring biocompatibility, extreme temperature stability (typically -60°C to +200°C), and electrical insulation. Other elastomers, such as EPDM, FKM, or TPE, are selected when chemical resistance, cost, or specific mechanical properties take priority. FVG supports both tracks.
FVG's Elastomer and Silicone Solutions capability covers the full co-moulding spectrum, from LSR injection overmoulding to multi-material insert moulding and 2K/3K processes. The key process specifications are:
Parameter | FVG Specification |
|---|---|
Dimensional tolerance | 0.08–0.15 mm for LSR components |
Silicone film thickness | Down to 0.08 mm (±10%) for ultra-thin overmoulding |
Cleanroom environment | ISO 14644 Class 7 & 8 (Class 8 & 9 for elastomers) |
Certifications | ISO 13485, FDA 21 CFR 820, IEC 60601 |
IP rating capability | Up to IP6X (dust-tight, engineered to IEC 60529) |
Substrate compatibility | Thermoplastics, metals, populated PCBs |
Liquid Silicone Rubber injection overmoulding is FVG's primary process for IoT applications requiring biocompatibility, electrical insulation, or wide operating temperature ranges. LSR's platinum-catalysed curing chemistry produces a covalently bonded interface with thermoplastic substrates, eliminating delamination risk under repeated thermal cycling. For a deeper look at the process, FVG's LSR injection moulding guide covers material selection, tooling considerations, and production readiness.
FVG's LSR injection process supports tight-tolerance components with complex geometries, including thin-wall overmoulded sensor housings, flexible connector seals, and soft-touch interface overlays for ruggedised IoT control panels.
Beyond LSR, FVG engineers across a full material portfolio to match the specific environmental and mechanical demands of each IoT application:
EPDM: Preferred for outdoor IoT enclosures and telecom equipment requiring UV, ozone, and weather resistance across a -50°C to +150°C operating range.
FKM (Viton): Specified for industrial IoT sensors in chemical processing or oil and gas environments, offering outstanding resistance to fuels, solvents, and aggressive fluids up to +200°C.
NBR (Buna-N): Used in hydraulic and fluid-adjacent IoT instrumentation where oil and fuel resistance is the primary requirement.
CR (Neoprene): Selected for applications combining moderate chemical resistance with inherent flame retardancy.
Silicone Rubber (SR/VMQ): The standard choice for wearable IoT devices, medical-grade connected sensors, and any application requiring skin contact or sterilisation compatibility.
For IoT devices requiring rigid-flexible hybrid housings, FVG supports insert moulding (metal or plastic substrate placed in the mould prior to elastomer injection) and multi-shot 2K/3K processes. These techniques are particularly relevant for IoT products with integrated antenna windows, sealed connector ports, or ergonomic soft-grip overlays on handheld industrial devices.
FVG's IoT and Connected Device manufacturing capability maps directly to the overmoulding use cases where silicone and elastomeric encapsulation add the most engineering value.
Industrial sensors deployed in manufacturing, energy, and logistics environments require enclosures that survive continuous vibration, chemical splash, and wide ambient temperature swings. FVG's elastomeric overmoulding delivers IP67/IP68-rated sensor housings with EPDM or FKM seals, protecting the underlying PCBA from ingress while maintaining dimensional stability across thermal cycles.
Relevant FVG process: LSR or FKM overmoulding on thermoplastic or aluminium sensor housings, with in-house PCBA assembly and functional testing completed before overmoulding.
Connected health devices, including ECG patches, remote patient monitoring modules, and biosensors, require skin-safe, biocompatible enclosures. LSR is the material of choice here, offering:
ISO 10993 biocompatibility compliance for skin-contact applications
Sterilisation compatibility (autoclave, EtO, gamma)
Flexibility and comfort for long-wear form factors
Sweat and UV resistance for fitness and outdoor wearables
FVG's ISO 13485-certified cleanroom manufacturing environment supports these applications at both prototype and production scale.
Outdoor IoT nodes, antenna enclosures, and smart metering equipment face weathering, UV degradation, and temperature extremes that standard thermoplastic housings cannot withstand alone. FVG applies EPDM and silicone overmoulding to create weatherproof gaskets, RF-transparent sealing layers, and shock-absorbing mounts for telecom infrastructure equipment.
FVG's case studies demonstrate silicone overmoulding capability at the precision end of the medical IoT spectrum. One documented application involves overmoulding an ultra-thin silicone film (0.08 mm ±10%) onto a nitinol wire mesh cone for a catheter-deployable cardiac occluder. While that application is not a standard IoT device, it illustrates the process precision available for connected medical devices requiring the same materials and tolerances.
Most elastomeric moulding specialists do not assemble electronics. Most EMS providers do not run LSR injection lines. FVG is unusual in holding both capabilities within a single manufacturing ecosystem, and for IoT product teams, that integration has concrete engineering implications.
FVG assembles IoT PCBs using SMT lines with high-frequency signal integrity controls, then transfers those assemblies directly to the moulding floor for overmoulding. This eliminates the handling, transit, and re-inspection risk that accumulates when electronics and moulding are sourced from separate vendors.
Why this matters technically: Low-pressure overmoulding of populated PCBs requires injection pressures of 5–40 bar, compared to 600–1,200 bar for standard thermoplastic injection. Coordinating that process with the PCBA team in the same facility means the moulding parameters can be validated against the actual board population, not a generic substrate proxy.
FVG designs and fabricates moulds in-house, which directly impacts lead time and design iteration cycles. For IoT products in development, rapid prototyping of overmoulded enclosures is available without waiting on external tooling suppliers. This is particularly valuable during design-for-manufacturability (DFM) reviews, where mould geometry changes frequently as the enclosure design evolves.
For regulated IoT applications, including connected medical devices and healthcare wearables, FVG's ISO 14644 Class 7 and 8 cleanroom environments support contamination-controlled moulding. Validation processes cover dimensional verification, material testing, and application-specific performance testing, with documentation aligned to ISO 13485 quality management requirements.
Bottom line for procurement: Sourcing overmoulded IoT assemblies from a single vertically integrated partner reduces BOM complexity, shortens NPI timelines, and creates a single point of accountability for both electronics and enclosure performance.
Choosing between LSR silicone and an alternative elastomer is a functional engineering decision, not a preference. The table below maps the key selection criteria to the material options FVG supports.
Selection Criterion | LSR Silicone | EPDM | FKM (Viton) | NBR | CR (Neoprene) |
|---|---|---|---|---|---|
Temperature range | -60°C to +200°C | -50°C to +150°C | -20°C to +200°C | -40°C to +120°C | -40°C to +120°C |
Biocompatibility | Excellent (ISO 10993) | Moderate | Limited | Limited | Moderate |
UV/Ozone resistance | Excellent | Excellent | Excellent | Poor | Good |
Chemical/oil resistance | Good | Poor (oils) | Excellent | Excellent | Moderate |
Electrical insulation | Excellent | Good | Good | Moderate | Good |
Flame retardancy | Good | Moderate | Good | Poor | Inherent |
Relative cost | Higher | Low | High | Low | Moderate |
LSR is the right call when the IoT device involves any of the following: skin or body contact, sterilisation requirements, extreme temperature cycling, electrical insulation across the overmoulded layer, or regulatory compliance with FDA or ISO 13485. Wearable health monitors, connected diagnostic devices, and any IoT product deployed in cleanroom or food-processing environments fall into this category.
If the primary requirement is chemical or oil resistance (industrial IIoT in processing plants), weathering durability for outdoor infrastructure (EPDM), or cost optimisation on high-volume consumer IoT, an alternative elastomer often delivers better value than LSR. FVG's materials engineering team can advise on the optimal compound selection during the DFM phase.
IoT devices entering medical, industrial, or telecommunications markets carry regulatory obligations that extend to the manufacturing process, not just the finished product. FVG's quality infrastructure is built to support those obligations.
Certifications and standards applicable to overmoulded IoT manufacturing :
ISO 13485 - Quality management system for medical device manufacturing, covering elastomeric moulding, PCBA, and box build
FDA 21 CFR 820 - Quality System Regulation for devices entering the US market
IEC 60601 - Safety and performance standards for medical electrical equipment
ISO 14644 Class 7 & 8 - Cleanroom classification for contamination-controlled moulding
IEC 60529 (IP6X) - Ingress protection rating standard, with FVG precision moulding engineered to meet IP6X specifications for IoT devices
For IoT products that are not medical devices but still require documented process control, such as industrial sensors subject to IEC or UL standards, FVG's validation documentation and traceability processes provide the audit trail that procurement and quality teams need.
A note on design validation: FVG supports rapid prototyping of overmoulded IoT enclosures, which means design validation testing, including dimensional verification, adhesion testing, and environmental durability assessment, can be completed on production-representative tooling before committing to full production volumes. This is particularly relevant for IoT product teams running IQ/OQ/PQ qualification sequences.
Yes, FVG offers both: Silicone (LSR) overmoulding and broader elastomeric overmoulding are established capabilities, not add-on services.
Tolerances are production-grade: LSR components achieve 0.08–0.15 mm dimensional tolerances, with ultra-thin silicone film capability down to 0.08 mm.
IoT-specific integration is the differentiator: FVG assembles IoT PCBs and overmoulds the enclosure in the same facility, removing the split-vendor risk that typically complicates IoT hardware programmes.
Material selection is application-driven: LSR for biocompatibility and temperature extremes; EPDM for outdoor weathering; FKM for chemical resistance; the right answer depends on the device's operating environment.
Compliance is built in: ISO 13485, FDA 21 CFR 820, IEC 60601, and IP6X-capable moulding are standard, not optional add-ons.
Prototyping is available: In-house mould design and fabrication supports rapid iteration before production commitment.
IoT product teams evaluating overmoulding partners should ask two questions: can the partner handle both the electronics and the moulding, and can they validate the IP rating against the actual populated board? FVG answers both.
Discuss your elastomeric or silicone overmoulding requirement with FVG's engineering team.