resources
Why an End-to-End Box Build Partner Gives OEMs a Decisive Manufacturing Advantage

Published on 12th October 2026
For most OEMs, box build assembly is where fragmentation does the most damage. Boards arrive from one supplier, enclosures from another, harnesses from a third, and testing happens at a fourth site entirely. Each handoff is a potential quality gap, a schedule delay, and an accountability dispute waiting to happen.
Consolidating that entire scope under a single end-to-end partner changes the risk profile of the programme. Here are seven concrete advantages that integration delivers.
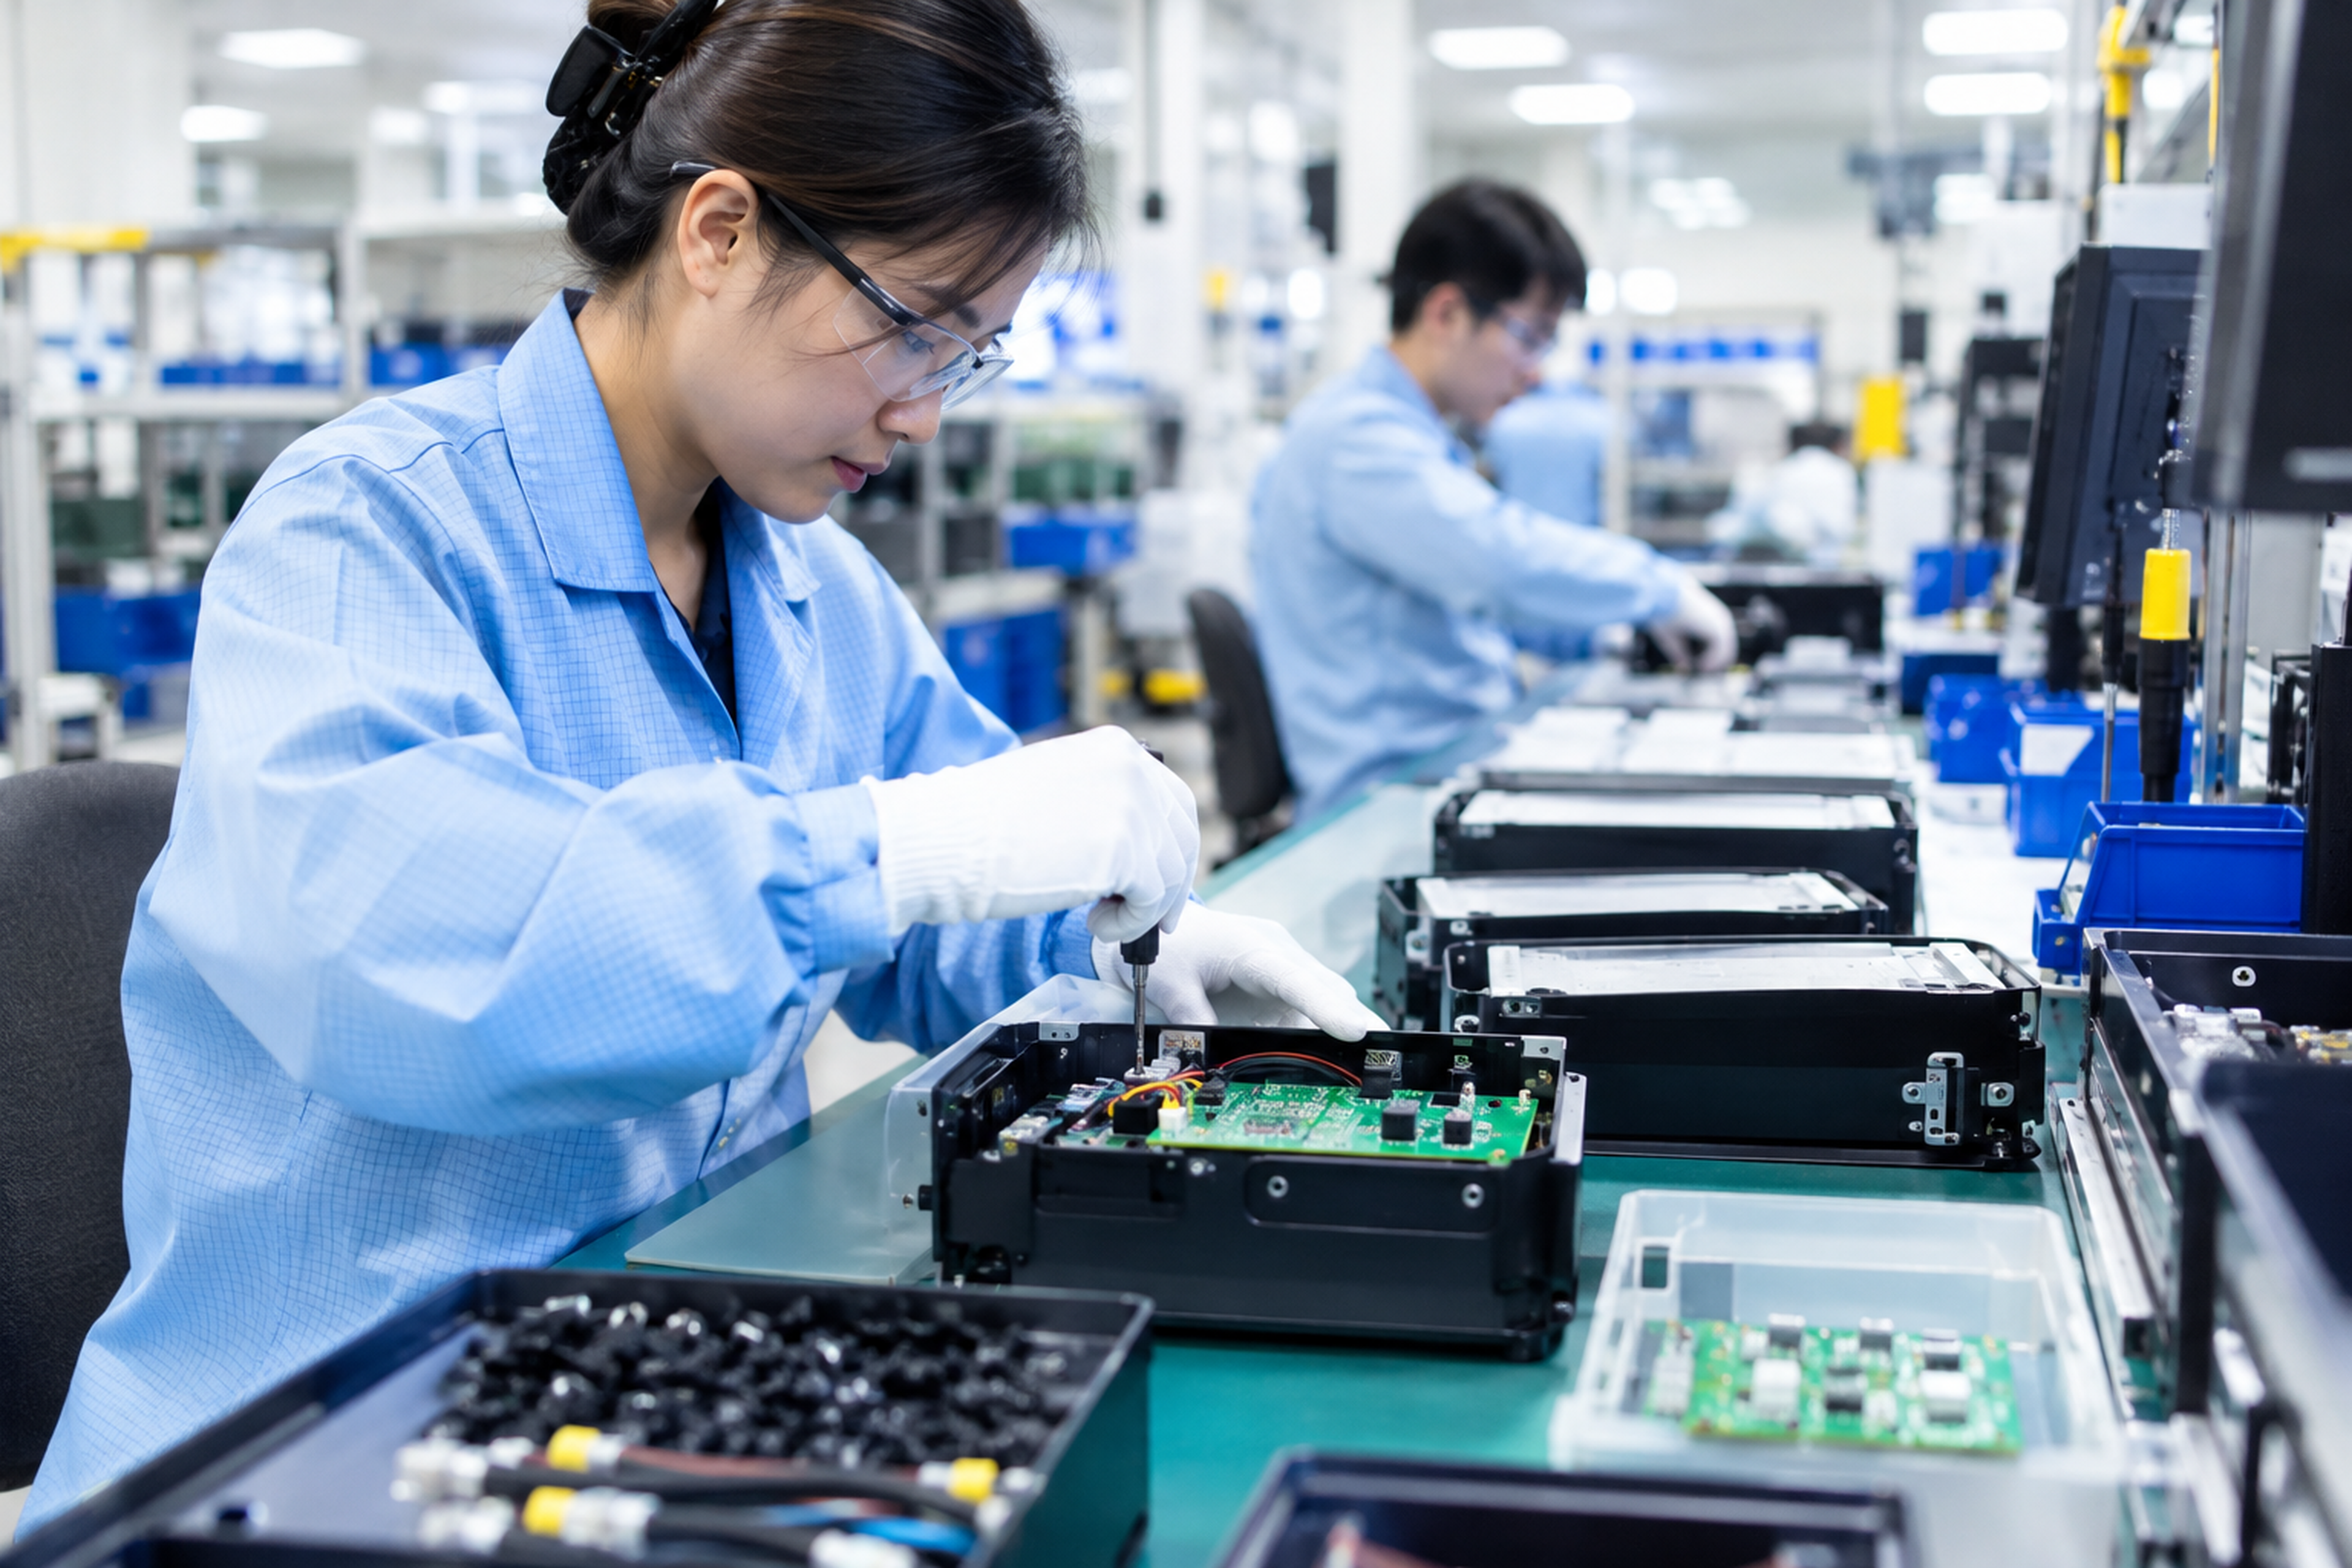
A single box build partner manages PCB integration, wiring and harness assembly, enclosure build, subsystem installation, system-level testing, and final packaging within one controlled facility. There are no inter-site shipments, no receiving inspections between stages, and no configuration drift between the build team and the test team. The workflow is continuous, not sequential across separate organisations.
An integrated partner engages before production begins. Design for manufacturability (DFM) and design for testability (DFT) reviews identify integration risks at the design stage, where corrections cost a fraction of what they cost in production. Harness routing is validated against the enclosure geometry. Test point accessibility is confirmed before PCB layout is finalised. Problems that would surface as field failures are resolved as design decisions.
In a multi-vendor model, each stage waits for the previous one to complete and ship. In an integrated model, enclosure preparation, harness fabrication, and PCBA validation run concurrently within the same facility. Industry benchmarks indicate this parallel execution reduces total programme lead times by 20 to 25% compared with sequential multi-vendor handoffs.
A single manufacturing execution system (MES) records torque values, solder profiles, firmware versions, and test results against individual serial numbers, across every stage from PCBA through to packaged unit. For OEMs operating under ISO 13485, IEC 60601, or FDA 21 CFR Part 820, this unified build record is a compliance requirement, not a convenience. A patchwork of records from four separate suppliers does not satisfy an audit.
In a fragmented model, system-level testing happens at the end of the supply chain, after all assembly is complete. In an integrated model, it functions as a continuous quality gate. Electrical continuity testing occurs at harness integration. In-circuit test (ICT) verifies the PCBA before enclosure assembly. Functional verification, environmental stress screening, and burn-in are managed by the same team that built the unit, with direct access to every process record.
Well-structured single-source box build programmes consistently achieve first-pass yield rates above 98%, with corresponding reductions in field return rates compared with equivalent multi-vendor programmes.
In a fragmented supply chain, a field return triggers a forensic investigation across multiple organisations, each with a natural incentive to identify the failure as originating elsewhere. An end-to-end partner carries full accountability. One engineering team understands the complete assembly. One quality system covers every stage. One point of contact is responsible for root cause analysis and corrective action.
Consolidation eliminates costs that multi-vendor models obscure: inter-vendor logistics, receiving inspection at each handoff, rework coordination across organisations, and the engineering time consumed by supplier disputes. Total programme cost reductions of 15 to 25% are achievable through consolidated supplier management, fewer rework cycles, and reduced logistics overhead.
The multi-vendor model distributes tasks but concentrates risk at the interfaces between suppliers. The integrated model concentrates scope with a single partner and distributes risk across a unified quality system, shared engineering team, and continuous traceability record.
For OEMs in medical device, industrial automation, and semiconductor equipment sectors, that distinction determines whether a programme meets its commitments or consistently absorbs resource in firefighting.
To discuss how FVG's box build and system integration capabilities can support your next programme, contact our engineering team.