resources
Plastic and Metal Hybrid Components: Engineering Reliability at the Interface
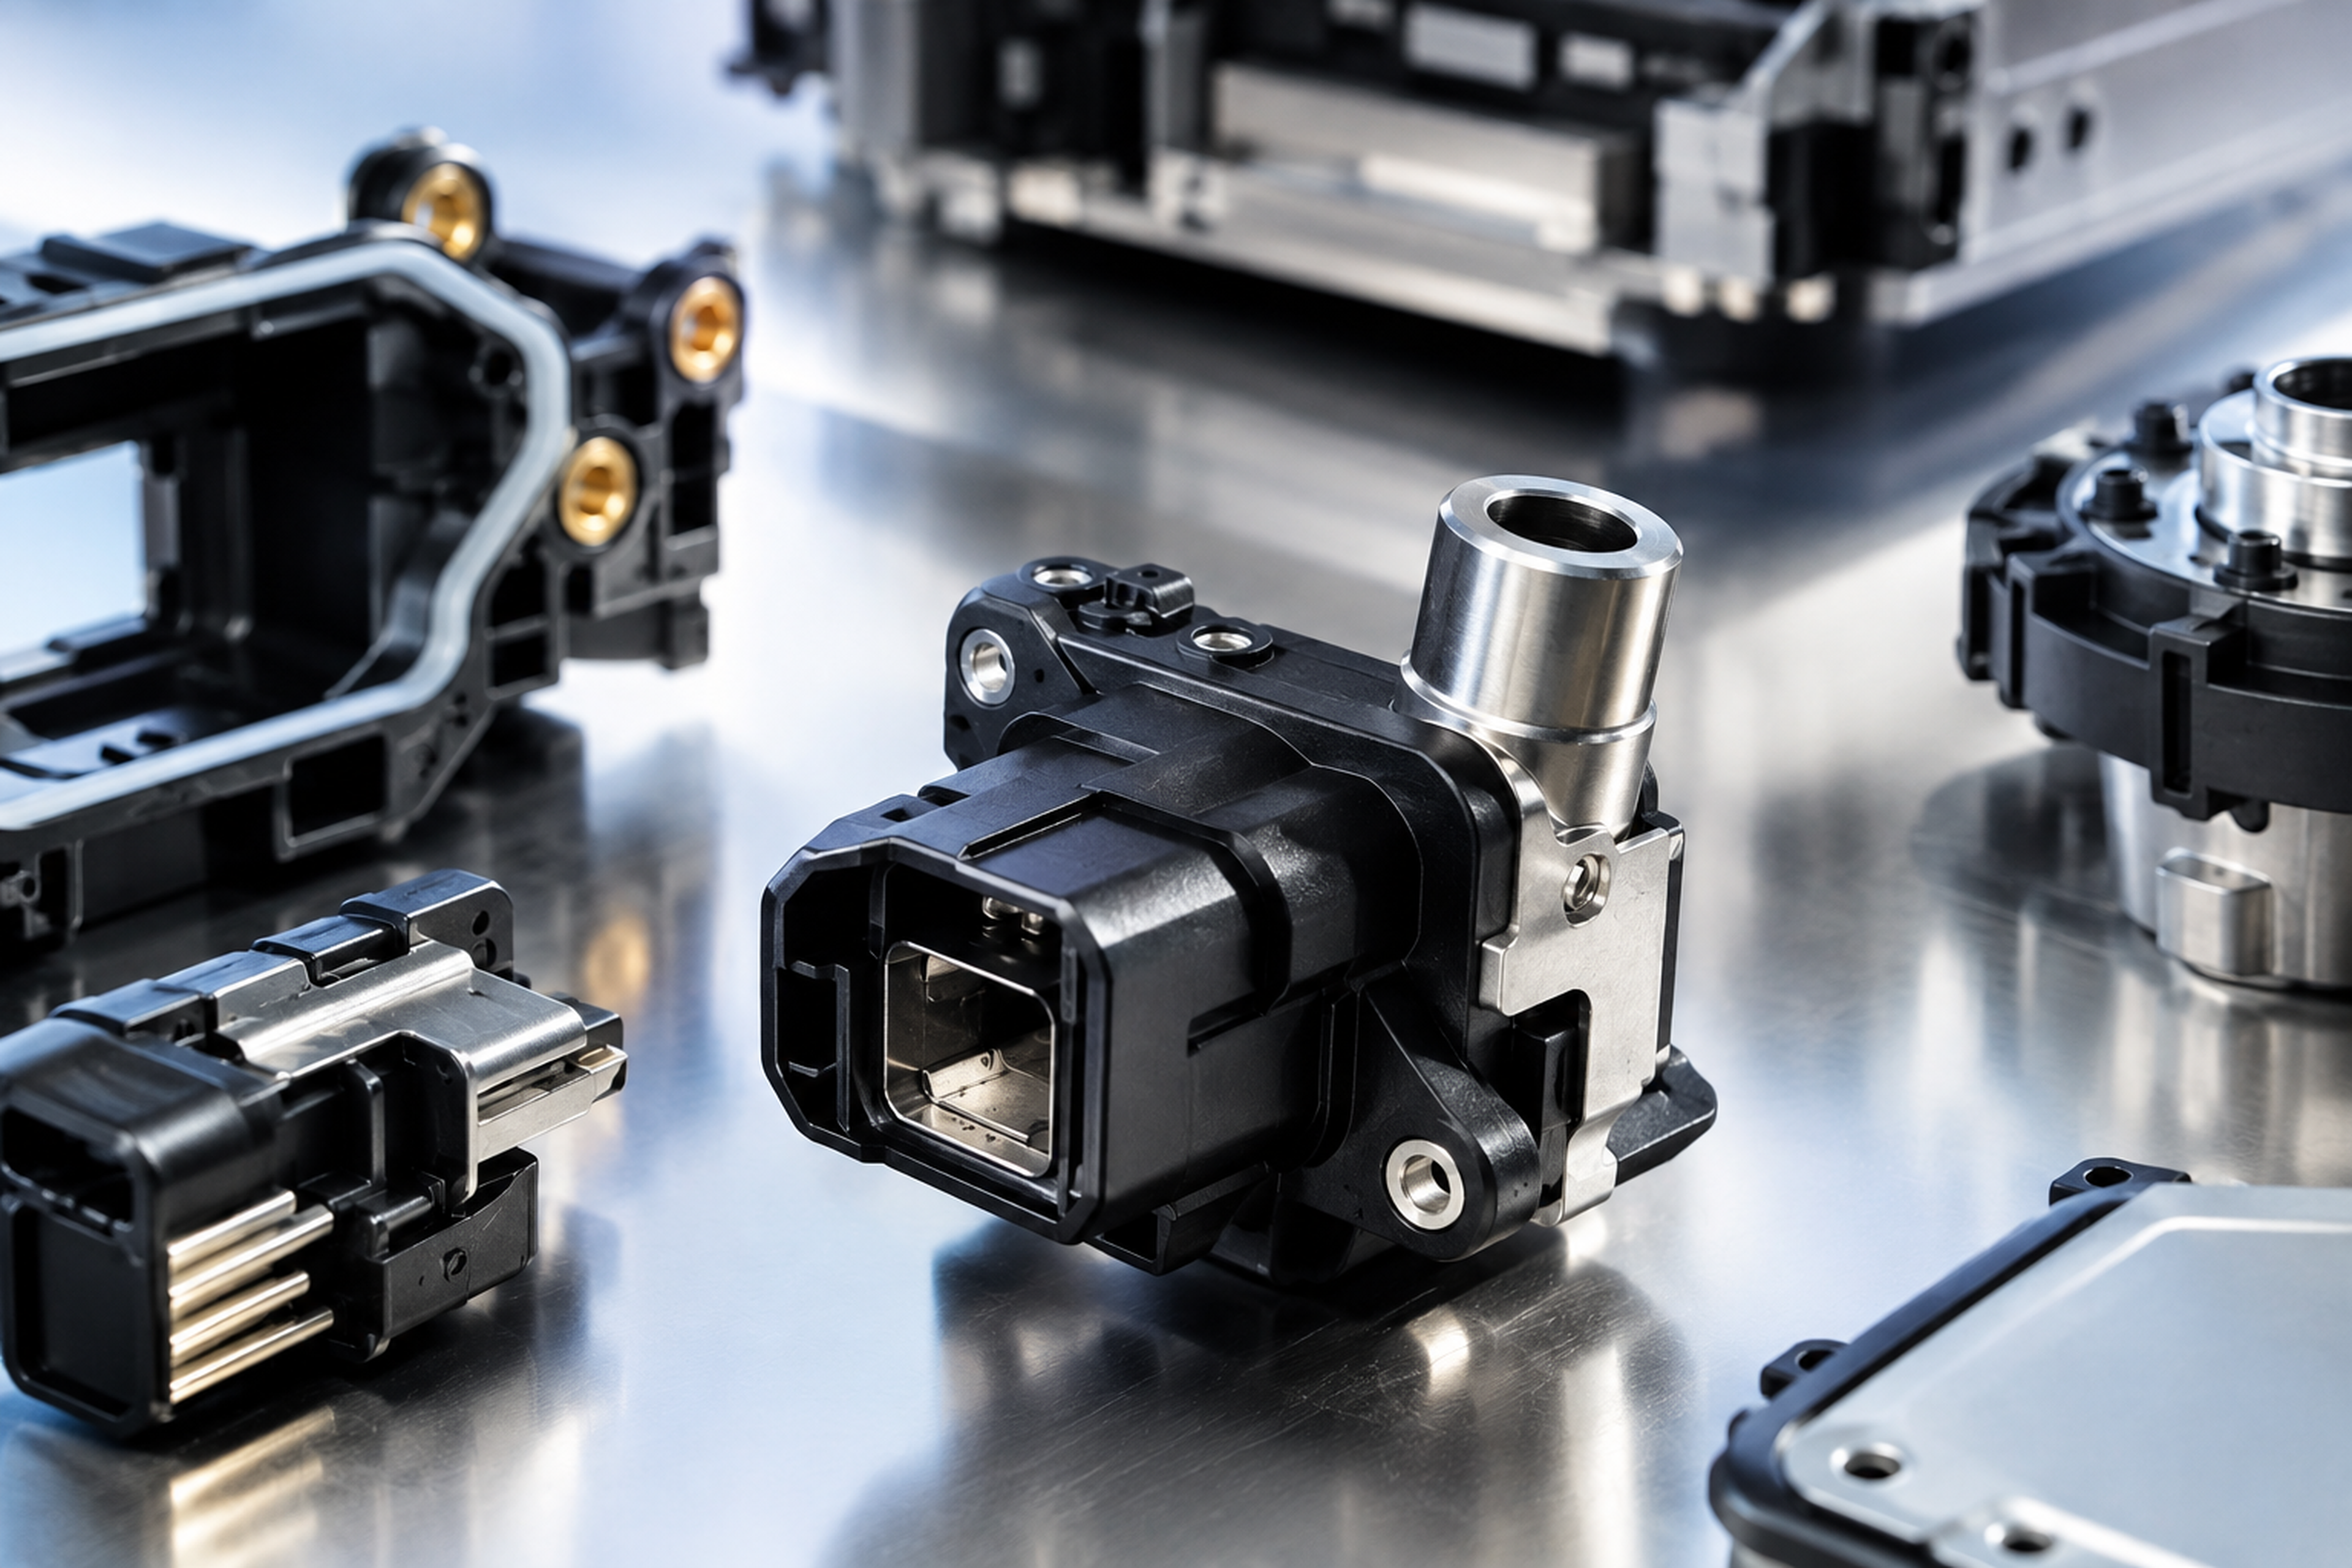

Published on 24th Sept 2026
Precision moulded components sit at the centre of modern manufacturing, and demand is still rising. The global injection moulding market was valued at USD 312.7 billion in 2025 and is projected to reach USD 462.5 billion by 2033, a compound annual growth rate (CAGR) of 5.1%, with Asia Pacific holding a 41.2% share. Within that market, the segment where plastic is moulded directly around metal is expanding faster: one estimate values custom insert moulding services at USD 1.21 billion in 2026, rising to USD 2.95 billion by 2035 at a 10.4% CAGR.
Growth, however, is not the same as reliability.
Combining plastic and metal in a single component is attractive because each material covers the other's weakness. Metal contributes strength, threads, conductivity and wear resistance. Plastic contributes geometric freedom, electrical insulation, low weight and cost efficiency at volume. But the two materials expand, contract and creep differently, and every hybrid part contains an interface where those differences meet. The core problem: in plastic-and-metal components, field failures rarely start in the plastic or the metal. They start at the boundary between them.
Flexi Versa Group (FVG) is a vertically integrated manufacturing partner based in Malaysia, with more than three decades of experience across moulding, precision metal work and system assembly. This article explains where plastic-metal hybrid components fail, why a single, integrated manufacturing programme controls those failure points better than a fragmented supply chain, and how FVG engineers reliability into the interface from the first design review.
Metals and plastics respond to temperature at very different rates, and the stress that results is locked into the part as it cools in the mould. Wall thickness is often treated as the safeguard, but thermal mismatch is the primary driver of cracking: where the coefficients of thermal expansion (CTE) of the resin and insert differ by more than roughly 20 µm/m·°C, even a 3 mm wall can crack on cooling. The same source notes that repeated thermal cycling in service generates cumulative fatigue at the interface, so a joint can pass first-article inspection and still degrade over its service life.
A joint that survives first assembly can still fail after thousands of thermal cycles.
A metal insert has to resist axial pull-out and rotational torque for the life of the product. Smooth cylindrical inserts do neither well. Knurls, grooves and undercuts create the mechanical lock that prevents loosening under vibration or cyclic stress, and placement matters as much as geometry: inserts positioned too close to a part edge risk cracking during ejection or under load, which is why guidance calls for a radial distance of at least twice the wall thickness around the insert.
Retention is a design decision that has to be made before the tool is cut, not after the first failed sample.
Even a sound design fails if the process is unstable. Interface voids form when moisture on an insert flashes to steam or a cold insert freezes the plastic before it fills the knurl features, and inserts can shift off their locating pins under injection pressure. Published good practice addresses both: preheating inserts to 80-120°C and holding pin-to-bore clearance to 0.01-0.03 mm.
Repeatability in the moulding cell is what turns a sound design into a reliable product.
Reliable hybrid components depend on a deep local ecosystem of materials, tooling, metalworking and finishing. Malaysia provides it.
Mature industrial ecosystem. Reliable access to raw materials, packaging, tooling and supporting processes shortens lead times and reduces logistics cost.
Port connectivity. Efficient ports at Klang and Penang support smooth shipping to North America, Europe and the Asia-Pacific region.
Supply chain diversification. Malaysia plays a central role in many "China+1" strategies, helping customers reduce exposure to tariff volatility and geopolitical risk.
Electronics-grade manufacturing base. Precision, contamination control and traceability are already standard expectations across the country's electronics supply chain.
Key insight: Malaysia exported US$151.07 billion of electrical and electronic equipment in 2025, which means suppliers of tooling, metal parts and finishing operate against electronics-grade tolerances as a matter of routine.
FVG's approach starts from a mechanical observation: the interface is only as controlled as the number of hands that touch it. When the metal component, the mould, the moulding process and the downstream assembly sit under one management system, the insert's specification, the resin's behaviour and the tool's condition can be engineered as a single system rather than negotiated between suppliers.
FVG runs injection moulding machines from 60 to 650 tons, many fitted with multiple core sequencers for complex geometries, and offers overmoulding and insert moulding that integrate metal inserts and multiple materials in a single component. On the metal side, FVG supplies precision-machined components and fabricated metal parts engineered for demanding equipment applications.
Process stage | FVG capability |
|---|---|
Metal components | Precision machining and fabricated metal parts |
Tooling | In-house tooling, local toolmaker partnerships, tool repair and modification |
Moulding | Insert moulding and overmoulding, 60 to 650 tons |
Handling | Robotic arms and automated handling |
Secondary processes | Spray painting, pad printing, screen printing, ultrasonic welding |
Assembly | Box build and ISO Class 7 and 8 cleanroom assembly |
Medical compliance | ISO 13485-certified moulding processes |
Insert and resin should be selected as a matched pair. A Design for Manufacturability (DFM) review at the concept stage addresses CTE compatibility, wall thickness around the insert, gate position, retention geometry and anti-rotation features while changes are still inexpensive. For the customer, this removes the most common cause of hybrid-part failure: a design that was validated as two separate parts and never as one.
Robotic arms and automated handling reduce human error and hold cycle times steady, which supports consistent insert positioning shot after shot. Consistent placement is what keeps insert location, bonding and wall thickness inside specification across a production run, not only in the first sample.
Hard metal inserts can abrade mould surfaces, and a worn tool produces dimensional drift at exactly the point where the plastic meets the metal. FVG's in-house tool repair, rectification and modification capability allows maintenance issues to be addressed quickly without waiting on external parties, reducing downtime and protecting dimensional stability during ramp-up and high-volume production.
Finishing and joining operations such as ultrasonic welding, printing and painting are carried out in-house, and box build integration follows within the same organisation. Fewer handoffs mean fewer opportunities for handling damage, specification drift or contamination at the finished interface.
Operational reality: every supplier handoff is a point where an insert specification, a tool revision or an inspection criterion can drift. Consolidating the sequence removes the handoffs rather than managing them.
Insert-moulded and overmoulded components combine metal strength with polymer geometry in compact, high-consistency parts. FVG's ISO 13485-certified moulding processes support compliant medical component production, where traceability is as important as tolerance.
Connectors, switches and structural fittings are typical insert-moulded applications, where the metal provides conductivity or load-bearing threads and the plastic provides insulation and form. These programmes need consistent quality across high volumes and traceability across batches, both of which depend on stable process control.
Equipment programmes often combine precision-machined metal components, moulded parts, cable harnesses and cleanroom assembly. FVG's semiconductor manufacturing capabilities include ISO Class 7 and 8 cleanroom assembly and precision-machined components, so hybrid parts can be built and integrated within a contamination-controlled workflow.
A fragmented supply chain treats the plastic part, the metal part and the assembly as separate purchasing decisions. Hybrid components do not behave that way in service. The table below maps the most common failure modes to the mechanisms that address them.
Risk | FVG approach |
|---|---|
Cracking from thermal mismatch | Resin and insert pairing reviewed at DFM stage, before tooling |
Insert loosening under vibration | Retention and anti-rotation geometry designed with the part |
Insert displacement or interface voids | Automated handling and controlled process in the moulding cell |
Mould wear from hard inserts | In-house tool repair, rectification and modification |
Handoff errors between suppliers | Moulding, secondary processes and assembly under one roof |
Tariff and geopolitical exposure | Malaysian manufacturing base within China+1 strategies |
The market opportunity is clear. Insert moulding and overmoulding are growing because they replace multi-part assemblies with single components that are stronger, lighter and faster to build.
The challenge is equally clear. Thermal mismatch, insert retention, process variation and tool wear all concentrate at the plastic-metal interface, and none of them can be corrected after the part has been moulded.
FVG addresses these risks through an integrated capability set:
DFM and material pairing. Resin, insert and geometry reviewed together before tooling begins.
Moulding capacity. Machines from 60 to 650 tons, with insert moulding and overmoulding.
Precision metal components. Machined and fabricated metal parts from the same group.
In-house tooling support. Tool repair, rectification and modification without external delay.
Secondary processes and assembly. Painting, printing, ultrasonic welding and box build under one roof.
Regulated and controlled environments. ISO 13485-certified moulding processes and ISO Class 7 and 8 cleanroom assembly.
The question is not whether plastic and metal belong together in the same component. They do. The question is whether the interface between them is engineered by one accountable team from the first design review, or discovered in the field.
Contact FVG to discuss your hybrid component programme, or explore FVG's precision plastic injection moulding capabilities.